Aluminium platform
AluCore
AluCore is the platform Lumax may consider for applications up to C5.
You are here

Lumax aluminium fixed-tilt platform
AluCore is Lumax Energy's aluminium-based fixed-tilt Ground Mount platform for commercial, industrial and utility-scale solar projects.
The system uses aluminium primary structural members and is available as a standard pre-engineered kit for suitable projects or as a custom-engineered structure. Lumax selects AluCore where the corrosion environment, structural layout, component handling, site conditions and project economics support an aluminium solution.
Platform evaluation
AluCore provides a distinct material route within the Lumax Ground Mount range.
Aluminium's corrosion behaviour and component mass can be advantageous where exposure is aggressive, where handling and assembly influence the construction plan, or where aluminium profiles allow the structure to be efficiently configured for the required support spacing.
Every site is assessed on its own terms. Wind loading, module geometry, foundations, terrain, component specification, installation method, supply strategy and total installed cost are assessed together before the platform is recommended.
The project is exposed to a more aggressive atmospheric corrosion environment and an aluminium platform is appropriate.
The required solution may extend up to C5 exposure, subject to the full environmental and engineering review.
R112 or R90 aluminium profile geometry provides a suitable support-spacing solution for the project loading.
Lower component mass or aluminium assembly characteristics support the planned construction method.
A standard AluCore kit falls within the site and loading parameters.
A larger project can benefit from a custom aluminium structure optimised around the module, layout, foundations and installation sequence.
AluCore uses aluminium primary members, while SteelCore uses steel. This affects material behaviour, member design, protection strategy, handling and commercial optimisation. The material choice cannot be separated from the complete structure.
Aluminium platform
AluCore is the platform Lumax may consider for applications up to C5.
Steel platform
SteelCore is positioned for C2 to C4 with an appropriate corrosion-protection system. SteelCore may offer the better project outcome where steel fabrication, structural efficiency and project scale favour an all-steel solution.
Lumax compares both platforms where either could meet the site requirement.
AluCore member options
R112 and R90 are aluminium purlin or profile options within AluCore. They are not separate Ground Mount products.
R112 is the normal AluCore profile and can be used for support spans up to 4 m where loading and project engineering permit. R90 is the less common option and is normally used where support spacing is 3 m or less. The final profile, span and overhang are determined by the module, wind loading, table geometry and structural calculations.
Normal AluCore profile
Support spans up to 4 m
Normal AluCore profile
Support spans up to 4 m where loading and project engineering permit.
Shorter-span profile
Where support spacing is 3 m or less
Shorter-span profile
Normally used where support spacing is 3 m or less.
Final profile, span and overhang are set by the module, wind loading, table geometry and structural calculations.
GM-01 · Confirmed AluCore arrangements
End elevations of the module arrangements supported by AluCore.
Schematic · Not to scaleSee what information helps Lumax assess each arrangement. A preliminary layout or preferred tilt is useful if available; you do not need a final design to start.
Two modules in portrait
Tilt range10° to 25°
2P Portrait
Share the module datasheet, preliminary layout and preferred tilt, if known. Lumax reviews module dimensions, loading and site conditions to establish the final table geometry and tilt.
Three modules in portrait
Tilt options10° or 15°
3P Portrait
If known, indicate whether the preliminary layout uses 10° or 15° and share the module datasheet. These are two design options; Lumax confirms the final arrangement against module dimensions, loading and site conditions.
Two east, two west
Tilt range10° to 15°
East-West / 4P
Show the intended east- and west-facing module arrangement in the preliminary layout, if available, and share the module datasheet. Lumax reviews module dimensions, loading and site conditions before confirming the final geometry.
Project conditions
Wind
Standard AluCore designs are available for SANS wind regions of 36 m/s and 44 m/s. The project location, loading, terrain and proposed array are reviewed to establish whether the standard design envelope applies. Where it does not, Lumax can develop a project-specific AluCore structure.
Terrain
North-South terrain is assessed for each project. East-West slopes of up to 3° can be accommodated, subject to the final project design, table arrangement and actual site conditions.
Corrosion
ISO 9223 classifies atmospheric corrosivity, while ISO 12944 uses environmental classification as an input to corrosion-protection decisions for steel structures. These standards provide context for the C2 to C5 language; they do not turn AluCore into a blanket 'C5-certified' product.
GM-02 · Corrosion exposure
Corrosion Positioning by Platform
Corrosivity categories used as selection context for AluCore and SteelCore.
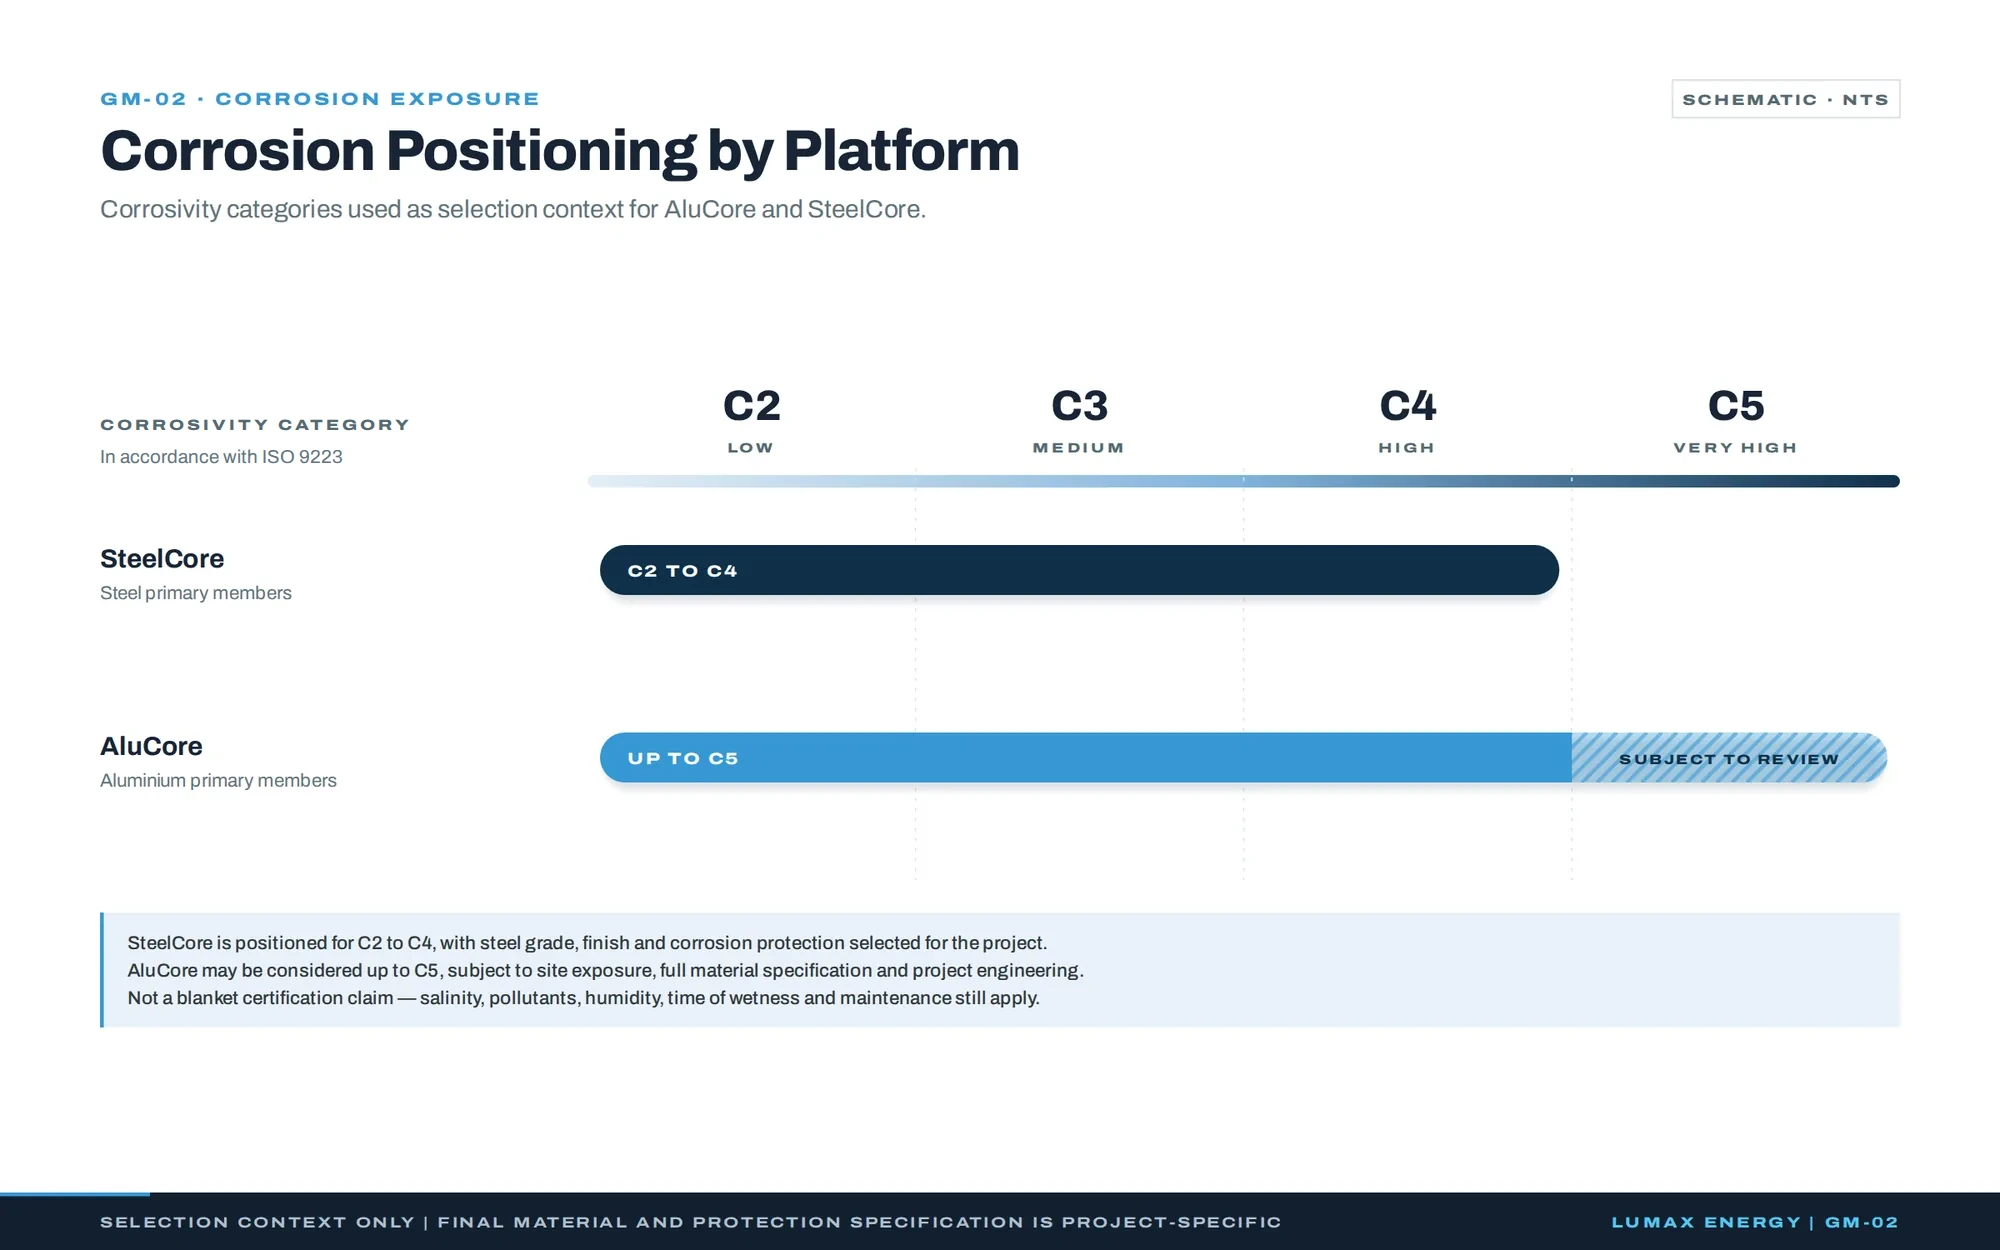
AluCore may be considered for applications up to C5, which represents a very high-corrosivity environment. The final recommendation still depends on the complete exposure, including salinity, pollutants, humidity, local microclimate, maintenance expectations, interfaces between materials and the detailed component specification.
GM-03 · One structural system
AluCore can be engineered with the foundation method that best fits the site and project. The full selection logic remains on the Ground Mount Hub.
Illustrative foundation routes, not supplied member, connection, anchor or reinforcement details. Final type, section, depth and installation are project-engineered. Not for construction.
For larger projects where the ground permits efficient, reliable pile installation.
01 · Direct-driven piles
Normally preferred for larger projects where ground conditions allow reliable installation. Direct driving is generally the fastest and most cost-effective method at scale, but it requires specialist piling equipment and verified site performance.
Where harder layers or local refusal make normal direct driving difficult.
02 · Pre-drilled and driven piles
Used where direct driving is difficult but a driven-pile solution remains practical. Pre-drilling assists installation through harder layers or local refusal conditions while retaining the pile-based foundation approach.
Where a driven-pile solution is not practical and drilled, concreted supports are required.
03 · Drill-and-concrete
Used where effective pile driving is not practical, particularly on larger sites where ground conditions require drilled holes and a concreted pile or post arrangement.
Where the soil, access and project requirements justify this approved higher-cost alternative.
04 · Ground screws
Foundation selection follows the site conditions and project design. Direct-driven piles are normally preferred for larger installations where ground permits. Ground screws provide an alternative where appropriate, usually at a higher cost.
For smaller projects or suitable standard-kit applications where specialist piling equipment is not commercially justified.
05 · Conventional concrete foundations
Normally considered for smaller sites and suitable standard-kit projects where mobilising specialist piling equipment would not be commercially justified. The civil foundation and structural anchoring scope must be clearly defined for the project.
Required site validation
Whenever direct-driven piles are selected, on-site pull-out testing is mandatory for every project and must be completed before manufacture.
The test confirms pile embedment and verifies the foundation assumptions used in design.
This requirement applies to AluCore and SteelCore alike. It is determined by the foundation route, not the structural material.
Sequence for direct-driven piles
Direct-driven pile foundation selected
On-site pull-out testing completed
Pile embedment confirmed and foundation design assumptions verified
Manufacture proceeds
Commercial and technical route
GM-06 · Commercial and technical route
Project inputs
Within the approved standard design envelope?
Yes
Standard AluCore kits are available for common configurations, subject to availability and the project falling within the approved design parameters. This is often the most practical route for projects of approximately 1 MW and smaller.
No · or scale justifies optimisation
For projects above approximately 1 MW, a custom-engineered AluCore structure is generally more cost-effective because the module layout, table length, R112 or R90 selection, support spacing, member sizes, foundations and material utilisation can be optimised across the full site.
Scale creates the opportunity to optimise
Larger projects may still use standard kits. Lumax compares both routes before recommending the better project outcome. The lowest-cost member is not necessarily the lowest-cost installed solution.
Lumax can begin platform assessment and prepare a preliminary quotation before complete geotechnical information is available. The initial work can use the project location, capacity, module datasheet, proposed layout, tilt and clearly stated assumptions to assess configuration, likely profile selection, standard-kit suitability and preliminary foundation routes.
The design and commercial basis are refined when the site and geotechnical information becomes available.
The applicable structural loading, material, connection, corrosion and project requirements are confirmed for the agreed scope and project location. The deliverables can include project drawings, structural calculations, foundation information, bills of material, installation information and professional engineering sign-off where included in the appointment.
AluCore questions
AluCore is normally considered where corrosion exposure, aluminium member geometry, component handling, site conditions and the complete installed project economics support an aluminium solution.
No. AluCore may be considered for applications up to C5, subject to the full environmental, material and engineering review. The recommendation still depends on salinity, pollutants, humidity, microclimate, maintenance expectations and component interfaces.
Both are AluCore profile options. R112 is the normal profile and can be used for support spans up to 4 m where engineering permits. R90 is less common and is normally used where support spacing is 3 m or less.
Yes. Lumax can begin with the project location, capacity, module datasheet, proposed layout, tilt and declared assumptions, then refine the design when site information becomes available.
It is mandatory whenever direct-driven piles are selected, regardless of whether the structural platform is AluCore or SteelCore, and must be completed before manufacture.
The current configurations are 2P portrait at 10° to 25°, 3P portrait at 10° or 15°, and East-West / 4P at 10° to 15°. Final geometry remains subject to module dimensions, loading, layout and project engineering.
A standard kit is often the most practical route for projects of approximately 1 MW and smaller when the site, loading, configuration and corrosion requirements fall within the approved design parameters. Lumax assesses suitability before recommending it.
Above approximately 1 MW, custom engineering is generally more cost-effective because profile selection, table length, support spacing, member sizes, foundations and material utilisation can be optimised repeatedly across the full site.
Send Lumax the project location, approximate MW size, module datasheet, preliminary layout, preferred configuration and tilt, available geotechnical or topographical information, corrosion requirements and relevant tender documents. Lumax will assess whether a standard AluCore kit or custom-engineered structure offers the better project outcome.